
Why Polish Stainless Steel?
When clients ask us how is stainless steel polished in a metal fabrication plant, they often wonder why we spend so much time on the finishing stage. Polishing isn’t just about making the metal look sleek and reflective; it radically improves the material’s performance, longevity, and hygiene.
By refining the surface, we eliminate microscopic peaks and valleys where moisture, chemicals, and bacteria love to hide.
Preventing Corrosion and Contamination
Raw stainless steel has a natural protective oxide layer, but fabrication processes like welding and cutting can disrupt it. Polishing restores and enhances this protection.
- Eliminates Pit Corrosion: Smooth surfaces prevent stagnant water and corrosive agents from trapping on the metal.
- Stops Bacterial Growth: In sanitary environments, a polished surface prevents microscopic bacteria from clinging to the steel, making cleaning fast and effective.
- Enhances Passivation: A cleaner, smoother surface allows the chromium oxide protective layer to reform uniformly.
Critical Industrial Applications

High-quality steel finishes are non-negotiable across global industries. We regularly polish fabrications for sectors with zero tolerance for contamination:
| Industry | Primary Requirement | Common Application |
|---|---|---|
| Pharmaceutical | Ultra-smooth surfaces to prevent batch cross-contamination. | Mixing tanks, piping systems, and storage vessels. |
| Food & Beverage | Sanitary finishes that withstand aggressive washdowns. | Commercial kitchen equipment, dairy processing lines. |
| Chemical Processing | High corrosion resistance against harsh acids and gases. | Heat exchangers, pressure vessels, and transport tanks. |
| Architecture | Aesthetic uniformity and resistance to environmental weathering. | Handrails, facades, and public structural elements. |
Surface Defects Removed During Polishing
Our polishing process acts as the ultimate quality corrector. Before shipping any fabricated structure, we use mechanical polishing to erase defects left behind during production:
- Weld Splatter and Discoloration: Removing the heat tint and slag caused by high-temperature welding.
- Deep Scratches and Gouges: Grinding out handling marks acquired during raw material transport.
- Scale and Mill Finish Imperfections: Stripping away the dull, rough outer layer from the steel mill to expose clean metal.
- Pitting and Porosity: Smoothing out tiny surface air pockets that could compromise structural integrity over time.
The Core Stainless Steel Polishing Process
In our metal fabrication plant, transforming a raw, heavily welded structure into a flawless piece of engineering requires a strict, methodical approach. We don’t just jump into making things shiny. The process relies on a precise abrasive grit sequence that starts with aggressive grinding and moves systematically toward fine finishing.
Here is how we break down the step-by-step mechanical polishing process on the shop floor:
- Step 1: Weld Blending (Grit 40 – 80): We start by attacking heavy weld beads, deep scratches, and surface scale. Using a high-torque angle grinder loaded with heavy-duty zirconia abrasive flap discs, we level the weld metal flush with the base material.
- Step 2: Intermediate Smoothing (Grit 120 – 240): Once the surface is flat, we transition to a pneumatic belt sander. This stage eliminates the deep scratches left by the initial grinding and begins to establish a uniform grain direction. If a client requests a specific directional texture, this is where the foundation for a premium stainless steel hairline surface treatment is laid.
- Step 3: Fine Finishing (Grit 320 – 400+): To prep for high-end applications or mirror finishes, we step up to ultra-fine abrasive pads. This eliminates any visible micro-scratches and brings the surface close to a reflective state.
Managing Heat and Surface Distortion
Stainless steel has low thermal conductivity and a high coefficient of thermal expansion compared to carbon steel. This means heat buildup during the industrial polishing process is a constant threat. If a technician stays in one spot for too long or applies too much pressure, the localized heat will cause severe warping, distortion, and localized discoloration (heat tint).
To prevent surface distortion, our fabricators keep the equipment constantly moving, utilize specialized lubricants to reduce friction, and carefully monitor the dwell time on thin-gauge materials. This discipline keeps the structural integrity perfectly intact while achieving the exact surface profile required.
Essential Tools for Polishing Stainless Steel
To achieve flawless surface finishes in our metal fabrication plant, we rely on a rugged, specialized toolkit. The right combination of machinery and abrasives ensures we cut down production time without compromising the metal’s integrity.
Heavy-Duty Leveling & Sanding Machinery
- Industrial Angle Grinders: Our go-to portable tools for aggressive weld blending, removing heavy burrs, and prepping tight corners.
- Stationary & Portable Belt Sanders: Essential for maintaining a consistent grain direction across long, flat sheets or tubular frames.
High-Performance Abrasive Grains
Choosing the correct grain prevents premature wear and surface scorching. We primarily stock two industrial powerhouses:
Zirconia Abrasive Flap Discs: Excellent for heavy stock removal and initial blending stages due to their self-sharpening properties.
Ceramic Grains: The premium choice for cool cutting on heat-sensitive alloys. Because stainless steel retains heat much more than softer metals—a key factor when analyzing the difference between aluminium and stainless steel processing—ceramic prevents warping and heat discoloration.
Buffing Wheels & Compounds
Moving from grinding to a high-gloss finish requires specialized coloring and buffing equipment:
| Equipment/Material | Primary Role in the Shop |
|---|---|
| Specialized Buffing Wheels | Cotton, sisal, or felt wheels used to buff out the micro-scratches left by fine sanding. |
| Solid Buffing Compound & Rouges | Applied directly to the spinning wheels. We progress from coarse greasy compounds for cutting to dry, fine rouges for the final reflection. |
| Industrial Lubricants | Formulated to reduce friction, manage heat buildup, and prevent the loaded abrasive from loading up with metal particles. |
Achieving Different Industry Surface Finishes

When we handle stainless steel fabrication for commercial spaces, architectural landmarks, or high-end retail, matching the exact surface finish specified in the blueprints is critical. We manipulate the grain direction and abrasive sequences to deliver distinct, industry-standard finishes that meet both aesthetic and functional demands.
Here is how we break down the two most requested architectural and industrial finishes:
- No. 4 Satin Finish: This is the classic brushed look. We achieve this by using a progressive abrasive grit sequence, typically finishing with a 120 to 150 grit belt. It creates uniform, linear directional lines that minimize the visibility of fingerprints and minor scratches. This clean, modern look is highly sought after for high-traffic environments, similar to our architectural metal installations at the Putian Wanda Plaza.
- No. 8 Mirror Finish: This is the most reflective finish possible. We completely remove all surface grain lines by starting with aggressive grinding and transitioning to ultra-fine felt pads or specialized buffing wheels. Combined with a high-grade buffing compound, the metal is polished until it acts as a flawless mirror. This ultra-premium look is perfect for luxury branding displays, much like the custom fabrication work we delivered for our jewelry brand store projects.
Standard Stainless Steel Finishes Comparison
| Finish Designation | Common Name | Abrasive Grit Used | Visual Appearance | Primary Applications |
|---|---|---|---|---|
| No. 3 | Intermediate | 60 – 100 Grit | Coarse, visible short grain | Food processing equipment, structural components |
| No. 4 | No. 4 satin finish | 120 – 150 Grit | Uniform, brushed linear texture | Kitchen appliances, handrails, architectural facades |
| No. 6 | Matte Satin | Tampico Brushed | Dull, soft satin finish | Architectural trim, non-reflective surfaces |
| No. 7 | Ultra-Satin | 180 – 240 Grit | High luster, slight reflection | Ornamental trim, elevator interiors |
| No. 8 | No. 8 mirror finish | 320 to Compounding | Flawless, highly reflective mirror | Luxury retail displays, decorative mirrors, signage |
Every project in our metal fabrication plant undergoes strict verification to ensure the finished piece perfectly aligns with client blueprints, maintaining consistent gloss levels and texture across all fabricated panels.
Quality Control and Surface Inspection
We don’t just rely on a quick glance to approve a finish. In our metal fabrication plant, ensuring the polished stainless steel meets precise specifications requires a mix of high-tech measurement and strict visual grading.
Measuring Surface Roughness (Ra Values)
To guarantee the surface meets strict hygienic or architectural standards, we use digital profilometers. These diamond-stylus tools trace the metal to calculate the exact surface roughness Ra value.
- No. 4 Satin Finish: Typically requires an Ra value between 0.5 to 1.5 microns.
- No. 8 Mirror Finish: Demands an ultra-smooth Ra value of under 0.1 microns.
| Finish Type | Typical Ra Range (Microns) | Primary Industrial Use |
|---|---|---|
| No. 4 Satin | 0.5 – 1.5 µm | Food processing, architectural panels |
| No. 8 Mirror | < 0.1 µm | Cleanrooms, mirrors, modern aesthetic effects |
Visual Inspection Techniques
Even with a perfect Ra reading, a panel can still have microscopic flaws. Our inspectors check every piece under high-intensity, multi-angle lighting to catch:
Subtle scratches or micro-pitting.
Uneven grain direction or mismatched reflectivity.
Weld blending shadows or cloudiness from improper buffing compound distribution.
The Essential Passivation Process
Mechanical polishing alters the top layer of the steel, dragging microscopic iron particles across the surface. To prevent future rust, every fabricated piece undergoes a thorough chemical cleanup.
Critical Step: We wash away all residual oils and buffing debris, then apply a specialized acid solution. This passivation process dissolves free iron from the surface, allowing the chromium to react with oxygen and rebuild its natural, corrosion-resistant passive layer.
Industrial Stainless Polishing FAQs
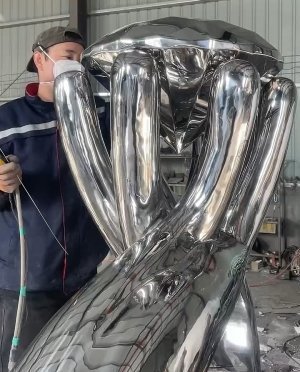
We get a lot of questions from clients and floor technicians about how we manage the stainless steel polishing process in our metal fabrication plant. Here are the direct answers to the most common queries.
1. Mechanical Polishing vs. Electropolishing
While both methods improve surface quality, they use completely different mechanisms to achieve their finishes.
| Feature | Mechanical Polishing | Electropolishing |
|---|---|---|
| Method | Physical abrasives (belts, wheels, flap discs) | Electrochemical bath (acid + electrical current) |
| Surface Impact | Cuts, flattens, and pushes the metal surface | Dissolves a microscopic layer of the base metal |
| Best Used For | Achieving specific grain directions like a No. 4 satin finish | Complex geometries, interior tubing, and ultra-clean surfaces |
| Contamination Risk | Can embed abrasive particles if not cleaned properly | Removes surface impurities entirely |
2. Why Does Polished Stainless Steel Sometimes Rust?
Stainless steel relies on a chromium oxide passive layer to resist corrosion. Mechanical polishing can temporarily disrupt this layer by exposing raw iron or embedding microscopic debris from an old abrasive grit sequence. If the steel is not properly cleaned or if it skips the passivation process, moisture can trigger localized pitting. You can read more about the chemical breakdown of why stainless steel rusts even after receiving high-grade surface treatments.
3. How Long Does It Take to Polish a Fabricated Structure?
There is no single timeline, as total shop hours depend on three main factors:
Starting Surface Condition: Heavy weld blending and deep scratches require extra time during the initial rough grinding stages using a zirconia abrasive flap discs or an angle grinder.
Target Specification: Stepping up from a standard No. 4 brush finish to a highly reflective No. 8 mirror finish doubles the processing time because of the multi-step buffing compound and rouge sequences required.
Geometry: Flat sheets pass quickly through a specialized belt sander, while complex architectural frames require manual labor to match the grain direction perfectly.
4. Essential Polishing Safety Precautions
Our fabrication plant enforces strict safety protocols to handle the hazards of metal finishing:
- Dust Extraction: High-volume vacuum systems capture fine airborne metallic dust and abrasive particles at the workstation.
- PPE Mandates: Technicians must wear heavy-duty face shields, respirator masks, and vibration-dampening gloves when operating a heavy angle grinder or belt sander.
- Fire Prevention: Aluminum and stainless steel dust can be explosive; we maintain dedicated workspaces and utilize spark arrestors to keep the polishing area safe.
- Ergonomic Rotation: Technicians rotate tasks regularly to prevent fatigue and hand-arm vibration syndrome (HAVS) from prolonged tool use.